A protective coating may look smooth and uniform from a distance, yet still contain tiny defects that compromise its performance.
One of the most overlooked defects in industrial painting is coating pinholes.
These small openings can appear in epoxy primers, high-build intermediate coatings, polyurethane topcoats and other protective coating materials.
Although some pinholes are difficult to detect with the naked eye, they can become potential pathways for moisture and corrosive substances to penetrate the coating film.
For steel structures operating in marine, coastal or industrial environments, this may increase the risk of premature corrosion.
However, not every surface pore is a through-film defect, and not every pinhole leads to immediate coating failure. The actual risk depends on the coating system, defect depth, exposure conditions and acceptance criteria.
Understanding the causes of coating pinholes is essential for improving coating quality, reducing rework and achieving more reliable corrosion protection.
In this article, we examine seven common causes of coating pinholes and practical ways to prevent them during industrial coating application.
1. Air Entrapment During Coating Application
One of the most common causes of coating pinholes is air trapped inside the wet coating film.
During mixing, pumping or spray application, air can become incorporated into the coating material.
As the coating begins to level and cure, trapped air may move toward the surface.
If the bubbles burst after the surrounding film has partially set, small openings or craters may remain.
The risk can increase when coatings are applied with unsuitable spray settings, excessive agitation or inadequate material preparation.
High-build epoxy coatings may be particularly sensitive to application conditions because of their viscosity and relatively thick wet films.
How to Prevent It
- Mix coating materials according to the manufacturer’s instructions.
- Avoid unnecessary high-speed agitation that introduces excessive air.
- Use appropriate spray pressure, nozzle size and equipment settings.
- Allow the specified induction time when required.
- Follow the recommended application thickness.
Controlling air entrainment helps reduce the likelihood of coating pinholes before the film begins to cure.
2. Solvent Entrapment and Excessive Film Thickness
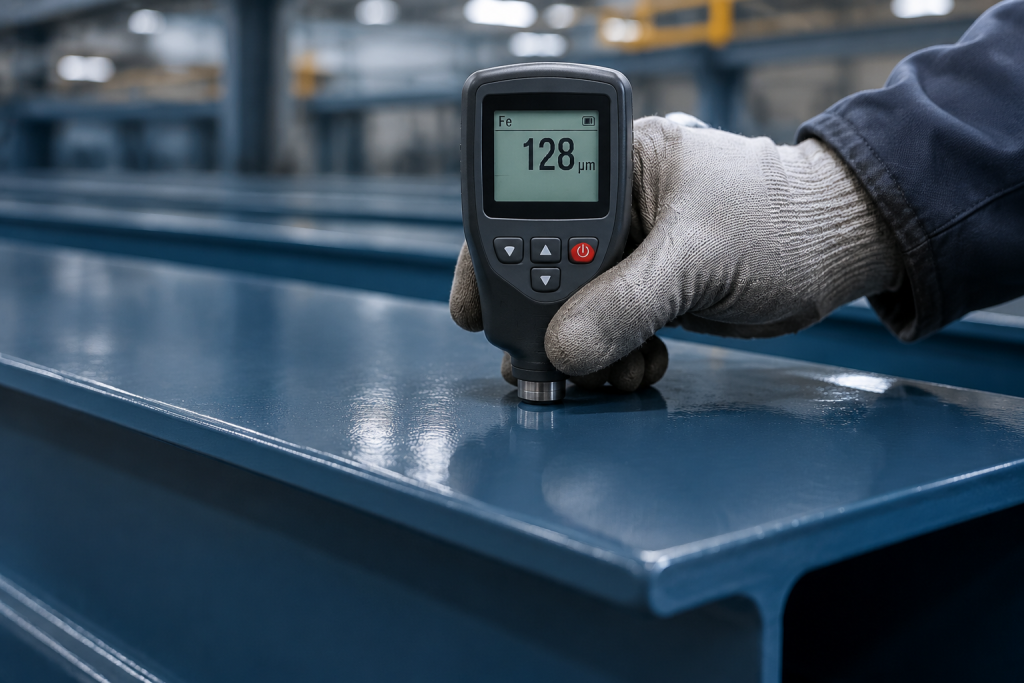
Applying more paint does not always produce better corrosion protection.
When a coating is applied excessively thick, solvents or other volatile components may have difficulty escaping from the film.
As the surface begins to dry or cure, material beneath it may continue releasing volatile components.
This can contribute to bubbling, pinholes and other film defects.
The risk depends on coating chemistry, solvent composition, temperature, ventilation and the actual wet film thickness.
For example, an epoxy intermediate coating applied far beyond its recommended thickness may not dry or cure as intended.
A thicker coating film is therefore not automatically a better protective barrier.
How to Prevent It
Monitor wet film thickness during application and verify dry film thickness after curing.
Use the manufacturer’s specified application range rather than attempting to achieve the entire system thickness in one excessively heavy coat.
Where multiple coats are required, observe the recommended recoat intervals.
A controlled coating build helps reduce the risk of coating pinholes associated with trapped volatiles.
3. Porous Steel Surfaces and Substrate Outgassing
Not all coating pinholes originate from the paint itself.
In some cases, the substrate contributes to the problem.
Porous surfaces, casting defects, rough welds and certain previously corroded areas may retain air or other gases.
When coating material is applied, trapped gases can escape through the wet film.
This process is commonly called outgassing.
Outgassing can become more pronounced when the substrate temperature rises during coating application or curing.
For example, a steel component exposed to direct sunlight may heat up while the coating is still wet.
As trapped gas expands, it can move through the coating and create small openings.
How to Prevent It
Inspect the substrate before painting.
Repair unacceptable surface defects and prepare welds according to the project specification.
Where outgassing is a known concern, consider application timing and substrate temperature trends.
Suitable sealing or application procedures may also be necessary for porous substrates, subject to coating manufacturer approval.
Proper substrate evaluation is an important step in preventing coating pinholes.
For protective coatings applied to metallic substrates, holiday detection can help identify discontinuities that may compromise corrosion protection. The testing principles are covered in ASTM D5162, which addresses discontinuity testing of nonconductive protective coatings on metallic substrates.
4. Incorrect Thinner Selection or Excessive Dilution
Industrial coatings are formulated to achieve a balance between viscosity, leveling, film formation and curing.
Adding the wrong thinner can disturb this balance.
An incompatible or excessively fast-evaporating solvent may contribute to surface defects under certain application conditions.
Excessive dilution may also reduce the solids deposited in each coat and affect the ability to achieve the specified dry film thickness.
For two-component epoxy and polyurethane systems, correct mixing and dilution are particularly important.
The appropriate thinner depends on the specific product formulation, spray method and ambient conditions.
How to Prevent It
Use only manufacturer-approved thinners.
Follow the recommended dilution range and mixing ratio.
Do not assume that the same thinner or dilution percentage is suitable for every epoxy primer, intermediate coat or polyurethane topcoat.
Always refer to the relevant technical data sheet.
Correct material preparation helps reduce coating pinholes and supports consistent film formation.
5. Surface Contamination Before Painting
Surface contamination can interfere with coating wetting and adhesion.
Common contaminants include:
- Oil and grease
- Dust and abrasive residue
- Soluble salts
- Moisture
- Silicone contamination
- Residual cleaning chemicals
Some contaminants can cause craters or fisheyes rather than true pinholes, but these defects may appear similar during a quick visual inspection.
Contamination can also create localized weaknesses in the coating system.
For example, oil residue on a steel surface may prevent the coating from wetting the substrate uniformly.
The result may be a visible crater or an area of inadequate film coverage.
How to Prevent It
Clean the substrate before abrasive blasting or mechanical preparation as required.
Remove dust and other residues before coating.
Check soluble salt contamination where the project specification requires it.
Confirm that the steel surface is dry and suitable for painting.
Surface preparation should be treated as part of the protective coating system rather than a separate cleaning task.
For additional information, see our guide to Surface Preparation for Steel.
6. Unsuitable Temperature, Humidity and Ventilation
Environmental conditions have a direct influence on coating application and film formation.
High temperatures may accelerate solvent evaporation and reduce the time available for proper leveling.
Low temperatures can slow drying or curing, depending on the coating chemistry.
High humidity may introduce additional risks, including condensation and moisture-related coating defects.
Inadequate ventilation can also affect solvent evaporation and worker safety.
For industrial painting projects, applicators should monitor:
Ambient Temperature
Confirm that the conditions fall within the coating manufacturer’s recommended range.
Substrate Temperature
Monitor the actual steel temperature, not only the surrounding air.
Relative Humidity
Follow the specified humidity limits.
Dew Point
Maintain the required separation between substrate temperature and dew point to reduce condensation risk.
For many protective coating specifications, a substrate temperature at least 3°C above the dew point is a common requirement, but the applicable product and project requirements must take priority.
Environmental control helps reduce coating pinholes and other defects associated with poor film formation.
7. Poor Spray Technique and Application Control
Even a well-designed coating formulation can develop defects when applied incorrectly.
Spray application requires control over several interacting factors:
- Spray pressure
- Nozzle size
- Spray distance
- Gun angle
- Overlap between passes
- Coating viscosity
- Application speed
- Wet film thickness
For example, excessive atomization or unsuitable equipment settings can contribute to poor film formation.
Applying paint too quickly may leave insufficient coverage.
Applying too much material in one pass may increase the risk of runs, solvent retention or localized film defects.
Complex steel structures create additional challenges because corners, welds and stiffeners can be difficult to coat uniformly.
How to Prevent It
Use spray equipment appropriate for the coating material.
Train applicators to maintain consistent spray distance, angle and overlap.
Inspect wet film thickness during application.
Apply stripe coats to critical edges and welds where specified.
Perform visual inspection before the next coating stage.
Good application control is essential for preventing coating pinholes and improving overall coating consistency.
Why Coating Pinholes Matter in Corrosion Protection
Protective coatings are designed to slow the movement of water, oxygen and corrosive substances toward the substrate.
A through-film pinhole may create a localized pathway through this protective barrier.
In environments containing chloride deposits and persistent moisture, such defects can increase the risk of localized corrosion.
However, the consequences depend on the coating system.
A small surface defect that does not penetrate the full coating film may have a different significance from a through-film holiday exposing the substrate.
This distinction is especially important in multilayer systems.
For example, a defect in a polyurethane topcoat does not necessarily mean that the epoxy intermediate coat and primer beneath it have failed.
Nevertheless, visible defects should be assessed against the project acceptance criteria rather than ignored.
Coating Pinholes vs. Blisters vs. Craters: What Is the Difference?
These coating defects are sometimes confused, but their causes and appearance can differ.
| Defect | Typical Appearance | Possible Causes |
|---|---|---|
| Pinholes | Small openings in the coating film | Trapped air, outgassing, volatile release |
| Blisters | Raised bubbles beneath or within the film | Moisture, osmotic effects, trapped volatiles, adhesion problems |
| Craters / Fisheyes | Circular depressions or areas of poor wetting | Surface contamination, silicone, wetting problems |
| Holidays | Discontinuities exposing the underlying surface | Missed coverage, damage, through-film defects |
| Runs / Sags | Downward movement of wet coating | Excessive wet film thickness, poor application control |
Correct identification matters because the appropriate corrective action depends on the defect mechanism.
Simply applying another coat without identifying the cause may not solve the underlying problem.
How to Inspect Coating Pinholes
Coating inspection should be planned according to the coating system, service environment and project specification.
1. Visual Inspection
Inspect the surface under suitable lighting for visible pinholes, craters, blisters and other defects.
2. Dry Film Thickness Measurement
Measure DFT using an appropriate method and calibrated instrument.
DFT measurement helps verify coating build, but it does not establish that the film is free of pinholes.
3. Holiday Detection
Where specified, appropriate holiday detection methods can help identify discontinuities in nonconductive coatings over conductive substrates.
The selected test method and voltage must be suitable for the coating thickness, substrate and coating system.
Improper testing can damage the coating or produce misleading results.
4. Repair and Reinspection
Where defects exceed the acceptance criteria, repair them according to the approved procedure.
This may involve cleaning, localized surface preparation, feathering, recoating and subsequent inspection.
The repair method must be compatible with the existing coating system.
How GranBond Approaches Coating Quality
At GranBond, industrial coating performance is evaluated as a complete system.
A successful coating application requires more than selecting a suitable epoxy primer or polyurethane topcoat.
It also depends on:
Substrate Preparation → Material Mixing → Application Conditions → Film Thickness → Curing → Inspection
For marine structures, energy storage containers, commercial vehicles and industrial steel equipment, these factors work together to influence long-term corrosion protection.
GranBond provides industrial coating solutions for different substrates and service environments, including epoxy primers, high-build epoxy intermediate coatings and weather-resistant topcoats.
Product selection and application procedures should be based on the actual project requirements.
Frequently Asked Questions
What causes coating pinholes in epoxy paint?
Common causes include air entrainment, substrate outgassing, solvent entrapment, excessive film thickness and unsuitable application conditions.
Can coating pinholes cause corrosion?
Through-film pinholes can create pathways for corrosive substances to reach the substrate. The actual risk depends on defect depth, coating system and exposure conditions.
Can a second coat cover pinholes?
In some cases, additional coating may restore coverage, but the defect must first be evaluated. Simply recoating without addressing the cause can result in recurring problems.
Are coating pinholes the same as holidays?
Not always. A pinhole is a small opening or pore, while a holiday is a discontinuity in the protective coating that may expose the underlying surface. A through-film pinhole can constitute a holiday.
How can coating pinholes be detected?
Visual inspection and suitable holiday detection methods may be used, depending on the coating system and project requirements.
Conclusion: Preventing Coating Pinholes Requires Process Control
Coating pinholes may appear small, but they can reveal important problems in surface preparation, material handling or application control.
Preventing these defects requires attention to the complete coating process.
The most effective approach combines appropriate substrate preparation, correct mixing, controlled application thickness, suitable environmental conditions and inspection.
For industrial structures exposed to demanding environments, reliable protection depends on achieving a continuous, properly applied coating system.
Need a More Reliable Industrial Coating System?
GranBond provides protective coating solutions for marine structures, energy storage containers, modular equipment, commercial vehicles and industrial steel structures.
Contact our technical team to discuss coating selection, application requirements and corrosion protection solutions for your project.
GranBond — BUILT FOR HARSH ENVIRONMENTS.