Corrosion Protection Starts With a Coating That Stays Attached
When evaluating an industrial protective coating system, manufacturers often focus on visible performance indicators such as salt spray resistance, weather resistance, hardness, and Dry Film Thickness (DFT).
However, all these properties depend on one fundamental requirement:
Coating Adhesion.
A coating may have excellent corrosion-resistant raw materials, a carefully designed formulation, and sufficient film thickness. But if it cannot maintain a strong bond with the substrate—or between individual coating layers—the entire protective system can fail prematurely.
This is particularly important for:
- BESS containers
- Modular data centers
- Containerized equipment
- Heavy trucks and trailers
- Special-purpose vehicles
- Marine and offshore equipment
- Industrial steel structures
In these applications, Coating Adhesion should not be considered an isolated laboratory value. It is one of the foundations of long-term coating integrity.
1. What Is Coating Adhesion?
Coating Adhesion describes the ability of a coating to remain bonded to the surface underneath it.
In a simple single-coat system, this primarily means adhesion between:
Coating → Substrate
But heavy-duty corrosion protection systems commonly contain multiple layers:
Topcoat
↓
Intermediate Coat
↓
Primer
↓
Steel Substrate
Therefore, a complete system depends on both:
Substrate Adhesion — the bond between the primer and steel.
and:
Intercoat Adhesion — the bond between individual coating layers.
If either interface fails, the integrity of the complete protective coating system can be compromised.
2. Why Coating Adhesion Matters for Corrosion Protection
A protective coating works partly by separating the steel substrate from the surrounding environment.
When the coating remains continuous and firmly attached, it helps prevent:
- Water
- Oxygen
- Chloride ions
- Industrial contaminants
- Other corrosive media
from reaching the steel.
However, once adhesion is lost, defects can develop between the coating and substrate.
Moisture may then penetrate these weak areas and promote underfilm corrosion.
As corrosion progresses underneath the coating, additional loss of adhesion can occur.
The failure mechanism may develop as:
Poor Adhesion
↓
Local Coating Separation
↓
Moisture Penetration
↓
Underfilm Corrosion
↓
Blistering / Peeling
↓
Accelerated Coating Failure
This is why excellent salt spray performance alone cannot compensate for poor adhesion.
3. Surface Preparation Has a Direct Impact on Coating Adhesion
One of the most important factors affecting Coating Adhesion is the condition of the substrate before painting.
Steel surfaces may contain:
- Rust
- Mill scale
- Oil
- Grease
- Dust
- Moisture
- Soluble salts
- Welding contamination
- Existing unstable coatings
If these contaminants remain on the substrate, the primer may bond to the contamination instead of directly to the steel.
The coating may initially appear normal, but its long-term adhesion can be significantly reduced.
For many heavy-duty protective coating systems, abrasive blast cleaning to a specified cleanliness level such as Sa 2.5 may be required.
The appropriate preparation standard should always follow the coating specification and actual service environment.
4. Surface Profile Helps Create Mechanical Anchorage
Surface cleanliness is only part of the preparation process.
Abrasive blasting also produces microscopic peaks and valleys on the steel surface.
This is known as the:
Surface Profile / Anchor Profile
A suitable profile increases the effective surface area and allows the primer to mechanically anchor to the substrate.
If the profile is too low, mechanical anchorage may be insufficient.
If it is excessively rough, the coating may have difficulty adequately covering the profile peaks unless sufficient material is applied.
Therefore:
Surface preparation, surface profile, Coating Adhesion and DFT are closely connected.
They should not be evaluated independently.
5. Primer Selection Also Determines Adhesion Performance
The primer is the first coating layer applied to the prepared substrate.
Its role is not only to provide corrosion protection.
It also establishes the bonding foundation for the complete coating system.
Depending on the application, different primer technologies may be selected, including:
- Epoxy primer
- Epoxy zinc-rich primer
- Specialized primers for galvanized steel
- Other industrial anti-corrosion primers
The correct primer depends on:
Substrate + Environment + Application + Subsequent Coating Layers
For example, a primer designed for blasted carbon steel may not automatically provide the same performance on galvanized steel or aluminum.
This is why substrate compatibility should always be verified.
6. Intercoat Adhesion Is Just as Important
In a multi-layer protective coating system, excellent primer-to-steel adhesion is not enough.
Consider a typical system:
Epoxy Zinc-Rich Primer
↓
Epoxy MIO Intermediate Coat
↓
Weather-Resistant Topcoat
If the intermediate coat does not bond properly to the primer—or the topcoat does not bond properly to the intermediate coat—the system can still delaminate.
Several factors can influence intercoat adhesion:
- Recoat interval
- Surface contamination
- Excessive curing before recoating
- Incorrect mixing
- Incompatible coating systems
- Surface chalking
- Dust
- Moisture
For this reason, the recommended recoat window in the product Technical Data Sheet should be followed.
Cross-cut and tape testing are widely used to evaluate coating adhesion on suitable substrates. ASTM D3359 provides standardized procedures for assessing coating adhesion by tape testing.
7. Why Recoat Interval Matters
The surface condition of an existing coating changes as it cures.
Applying the next coat within the recommended recoat interval helps create reliable bonding between layers.
If the maximum recoat interval is exceeded, the previous layer may become too fully cured or contaminated to provide optimal intercoat adhesion without additional preparation.
Depending on the coating system, corrective preparation may include:
- Cleaning
- Removal of contaminants
- Light abrasion
- Surface roughening
before applying the next coat.
The exact procedure should follow the relevant product specification.
This is particularly important in multi-coat C5 systems where the performance of the complete system depends on each layer remaining firmly bonded.
8. Excessive DFT Can Affect Adhesion and Coating Integrity
Applying more paint does not automatically produce a stronger coating.
As discussed in our previous article on Dry Film Thickness, excessive coating thickness can create additional risks depending on the coating chemistry and application conditions.
These may include:
- Solvent entrapment
- Incomplete curing
- Increased internal stress
- Cracking
- Intercoat problems
If internal stress becomes greater than the strength of the coating/substrate or coating/coating interface, adhesion failure may occur.
Therefore, Coating Adhesion and DFT should be considered together.
The objective is to achieve the specified film thickness—not the maximum possible thickness.
9. How Is Coating Adhesion Tested?
Several methods are used to evaluate coating adhesion depending on the coating type, substrate, film thickness, and project requirements.
Two commonly encountered approaches are:
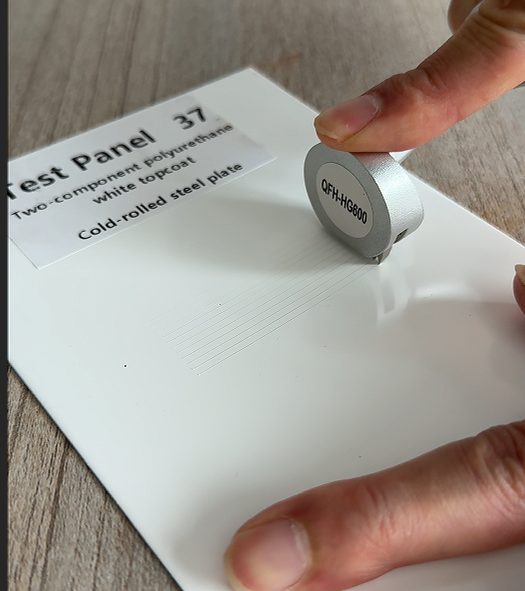
Cross-Cut Adhesion Test
A lattice pattern is cut through the coating using a suitable cutting tool.
The condition of the coating around the cuts is then evaluated according to the applicable test method.
Cross-cut testing is useful for comparing adhesion performance on appropriate substrates and coating systems.
Pull-Off Adhesion Test
A test dolly is bonded to the coating surface and pulled perpendicular to the substrate using specialized equipment.
The force required to separate the system is measured.
Pull-off testing can provide quantitative information about adhesion strength and can also help identify the location of failure within a multi-layer coating system.
10. Cross-Cut Results Must Be Interpreted Correctly
A cross-cut test is visually simple, but the result should not be interpreted without considering the test conditions.
Factors such as:
- Coating thickness
- Coating hardness
- Substrate
- Cutting tool
- Blade spacing
- Curing condition
- Test standard
can affect the result.
Therefore, statements such as:
“This coating passed the adhesion test.”
should ideally be accompanied by the relevant test method and test conditions when used as formal technical data.
This makes performance claims more meaningful and comparable.
11. Mechanical Impact Can Reveal Adhesion Weaknesses
A coating can appear well bonded under static conditions but behave differently after mechanical deformation or impact.
This is especially important for:
Heavy Trucks and Dump Bodies
Stone impact, cargo loading, vibration and structural movement continuously stress the coating.
BESS and Modular Equipment
Transportation, lifting and installation can create localized mechanical impact.
Industrial Equipment
Fabrication, assembly and maintenance may subject coated surfaces to mechanical stress.
For these applications, adhesion should be evaluated together with:
Flexibility + Impact Resistance + Coating Toughness
rather than as a single isolated property.
12. Different Substrates Require Different Adhesion Strategies
Not all metal substrates behave the same way.
Carbon Steel
Proper cleaning and abrasive blasting can provide an excellent foundation for many epoxy coating systems.
Galvanized Steel
The zinc surface requires appropriate cleaning and compatible primer selection.
Aluminum
The surface chemistry differs significantly from carbon steel and may require specific pretreatment and coating selection.
This is particularly relevant to manufacturers producing:
- Truck bodies
- Trailers
- Containers
- Equipment enclosures
- Special-purpose vehicles
where several different metals may exist within the same product.
A coating that performs well on carbon steel should not automatically be assumed to perform equally well on every metallic substrate.
13. Adhesion Is Part of the Complete Coating System
Long-term protective performance should be viewed as a chain:
Substrate Condition
↓
Surface Preparation
↓
Surface Profile
↓
Primer Compatibility
↓
Correct DFT
↓
Recoat Interval
↓
Intercoat Adhesion
↓
Topcoat
↓
Inspection
↓
Service Environment
A weakness at any stage can influence the final result.
This is why industrial corrosion protection should be approached as a system engineering problem, rather than simply a paint selection problem.
14. Coating Adhesion for Harsh Environments
The importance of Coating Adhesion increases when equipment operates under demanding conditions.
For BESS containers and modular data centers, the coating must tolerate outdoor exposure and temperature cycling.
For commercial vehicles, the coating must also withstand vibration, impact and deformation.
For marine and offshore structures, humidity and salt contamination increase the consequences of even small coating defects.
In every case, maintaining a strong bond between:
Steel → Primer → Intermediate Coat → Topcoat
helps preserve the integrity of the protective barrier.
For quantitative adhesion evaluation, ASTM D4541 describes pull-off testing methods used to determine the pull-off strength of coatings applied to rigid substrates.
Frequently Asked Questions
Why is Coating Adhesion important?
Coating Adhesion helps the protective coating remain firmly attached to the substrate and between individual layers. Poor adhesion can contribute to delamination, blistering, underfilm corrosion and premature coating failure.
What causes poor coating adhesion?
Common causes include inadequate surface preparation, oil, dust, moisture, soluble salts, incompatible primers, incorrect recoating, poor curing and unsuitable application conditions.
What is a cross-cut adhesion test?
A cross-cut adhesion test evaluates coating adhesion by cutting a defined lattice pattern through the coating and assessing the degree of coating separation according to a specified test method.
Is stronger adhesion always better?
High adhesion is important, but coating performance also depends on flexibility, toughness, DFT, corrosion resistance and compatibility between layers. The complete coating system should be evaluated.
Can good adhesion prevent corrosion?
Good adhesion contributes significantly to maintaining coating integrity, but it is only one part of corrosion protection. Surface preparation, coating formulation, film thickness, application quality and environmental exposure also influence service life.
Conclusion
Coating Adhesion is one of the foundations of a reliable industrial protective coating system.
A high-performance coating must do more than resist salt spray or maintain color under UV exposure.
It must remain firmly connected to the substrate and to every other layer throughout its service life.
Long-term adhesion depends on controlling:
- Surface preparation
- Surface profile
- Substrate compatibility
- Primer selection
- DFT
- Recoat interval
- Intercoat cleanliness
- Application conditions
- Mechanical properties
- Inspection
For BESS containers, modular equipment, commercial vehicles, marine structures and other industrial assets, strong adhesion helps ensure that the coating system can continue performing as a complete protective barrier.
The most reliable corrosion protection therefore begins with a simple principle:
A protective coating can only protect the steel as long as it remains securely attached to it.
About GranBond
GranBond develops industrial protective coating systems for commercial vehicles, containerized and modular equipment, marine and offshore structures, and other demanding steel applications.
Our coating development considers not only corrosion resistance, but also adhesion, impact performance, film thickness, weather resistance, application characteristics and long-term system compatibility.
GranBond — BUILT FOR HARSH ENVIRONMENTS.
CTA
Need Better Coating Adhesion for Your Application?
GranBond can evaluate coating systems according to your:
- Substrate
- Surface preparation
- Application environment
- Production process
- Required corrosion protection
- Mechanical performance requirements